
 EN
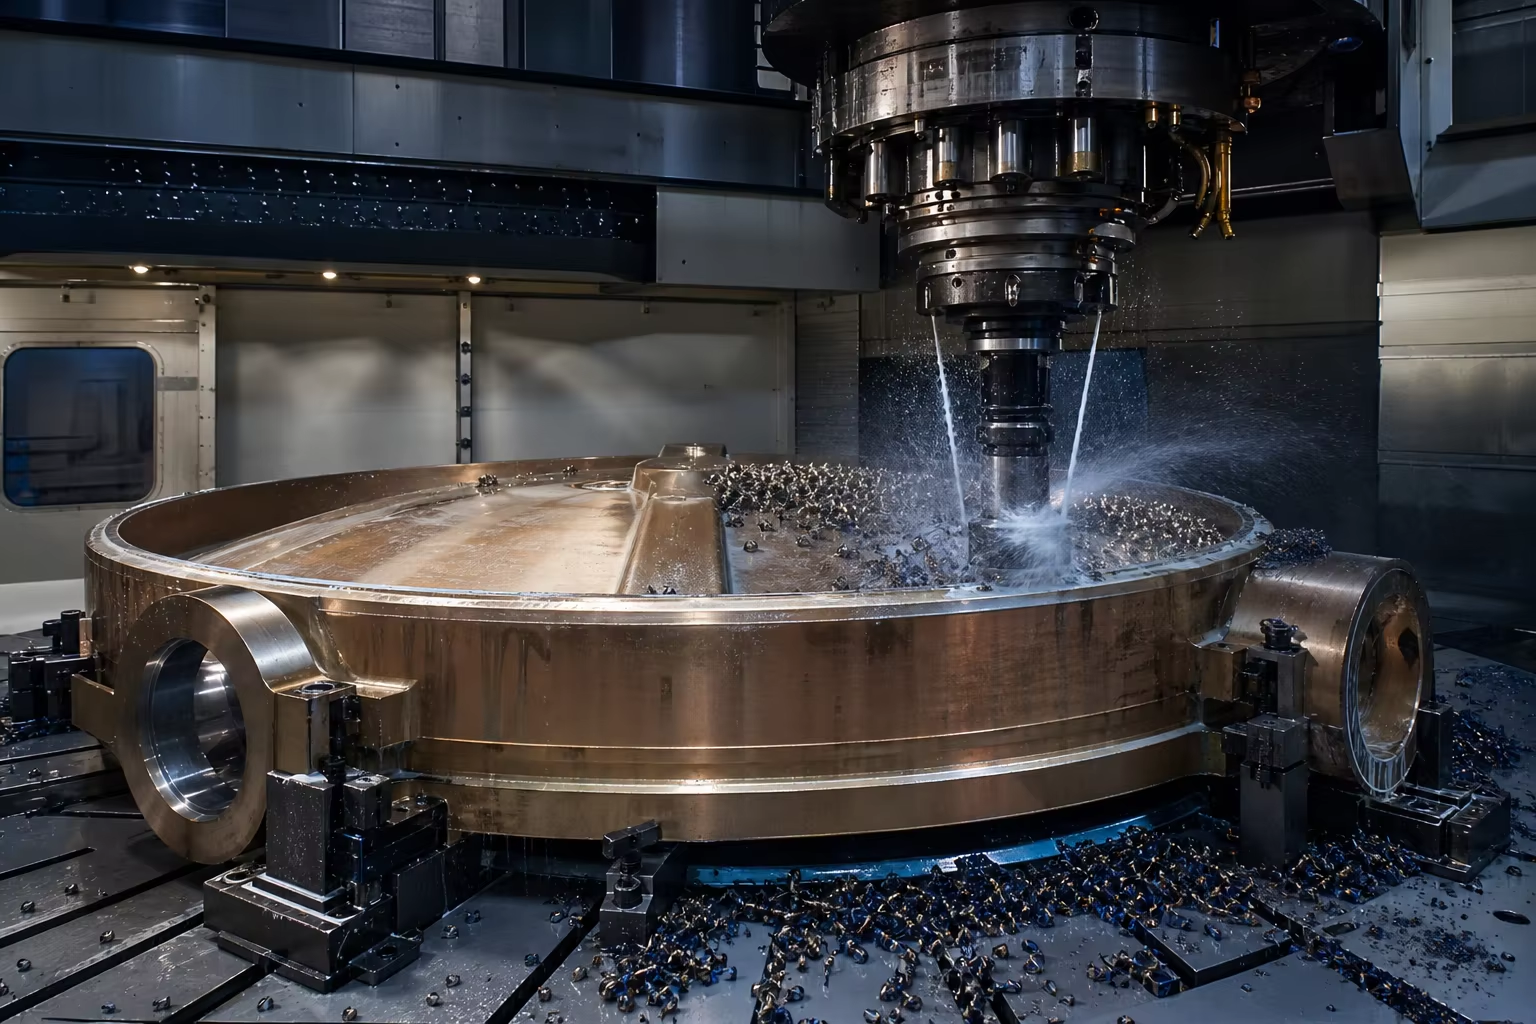
Meta Description: A comprehensive technical guide to large-diameter water treatment and seawater reverse osmosis (SWRO) desalination valve castings. Explore Ni-Resist austenitic ductile iron (ASTM A439 D-2), Aluminum-Bronze (ASTM B148 C95800), vulcanized EPDM lined ductile iron (EN-GJS-400-15), and large vertical CNC turning for DN600 to DN3000 valves.
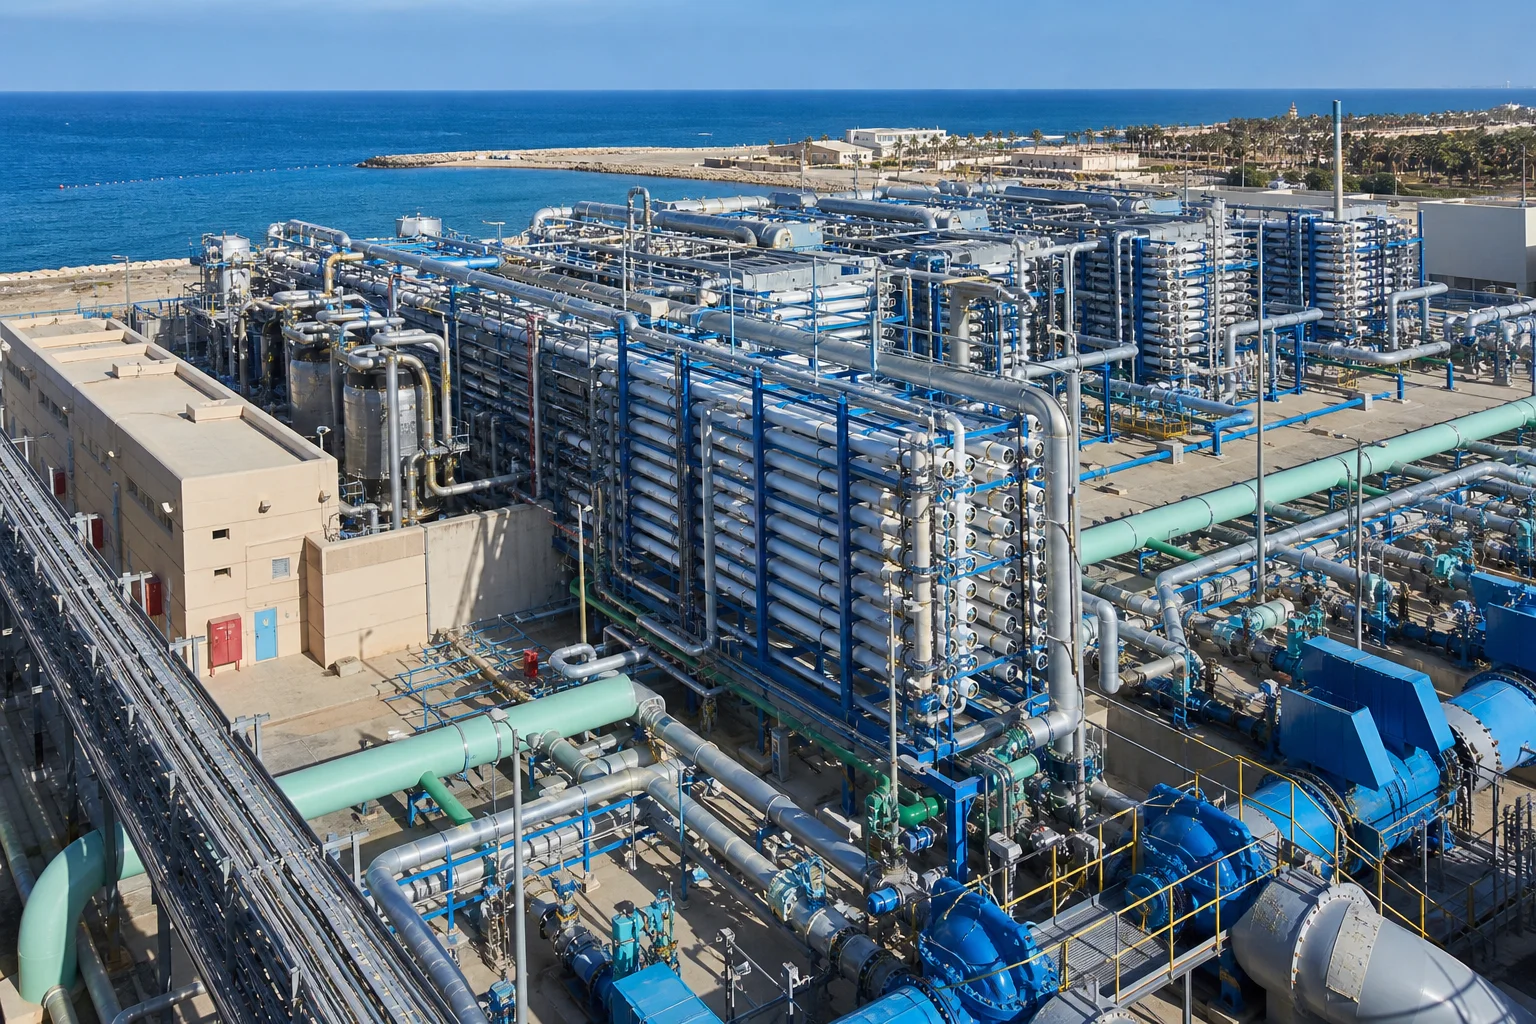
In municipal potable water networks, mega-scale wastewater treatment facilities, and seawater reverse osmosis (SWRO) desalination plants, large-diameter flow control valves operate as the primary hydraulic control infrastructure. Ranging in nominal pipe sizes from DN600 to DN3000 (), double-offset and triple-offset butterfly valves, gate valves, and check valves process hundreds of thousands of cubic meters of water per day under working pressures up to .
Operating under continuous high-flow hydraulic regimes, these massive valve castings face severe environmental and mechanical degradation:
- Seawater Reverse Osmosis (SWRO) Desalination: Raw seawater intake () and concentrated hypersaline brine reject streams () cause aggressive chloride crevice corrosion, pitting corrosion, and galvanic cell attack.
- High-Velocity Throttling & Cavitation: Turbulent flow through large valve discs creates micro-jet vapor implosion shock waves ( local pressure), eroding disc edges and body seating necks.
- Bi-Directional Bubble-Tight Sealing Standards: Governed by AWWA C504 (Rubber-Seated Butterfly Valves) and EN 593 / ISO 5752, large water valve castings must maintain zero-leakage shutoff under full reverse pressure head.
Surviving decades of corrosive water service requires specialized foundry metallurgy: casting Austenitic Ni-Resist Ductile Iron (ASTM A439 Type D-2 / D-2B) for brine pumps and valves, Nickel-Aluminum Bronze (ASTM B148 C95800 / EN 1982 CC333G) for marine intake valves, high-ductility Ferritic Ductile Iron (EN-GJS-400-15 / GB QT400-18) with precision-cast EPDM lining dovetail retention grooves, and executing precision vertical CNC turning of disc sealing hydrofoils.
This engineering guide provides an in-depth analysis of water and desalination alloy metallurgy, DFM casting design, large vertical lathe CNC machining, vulcanized elastomeric lining integration, and hydrostatic pressure testing.
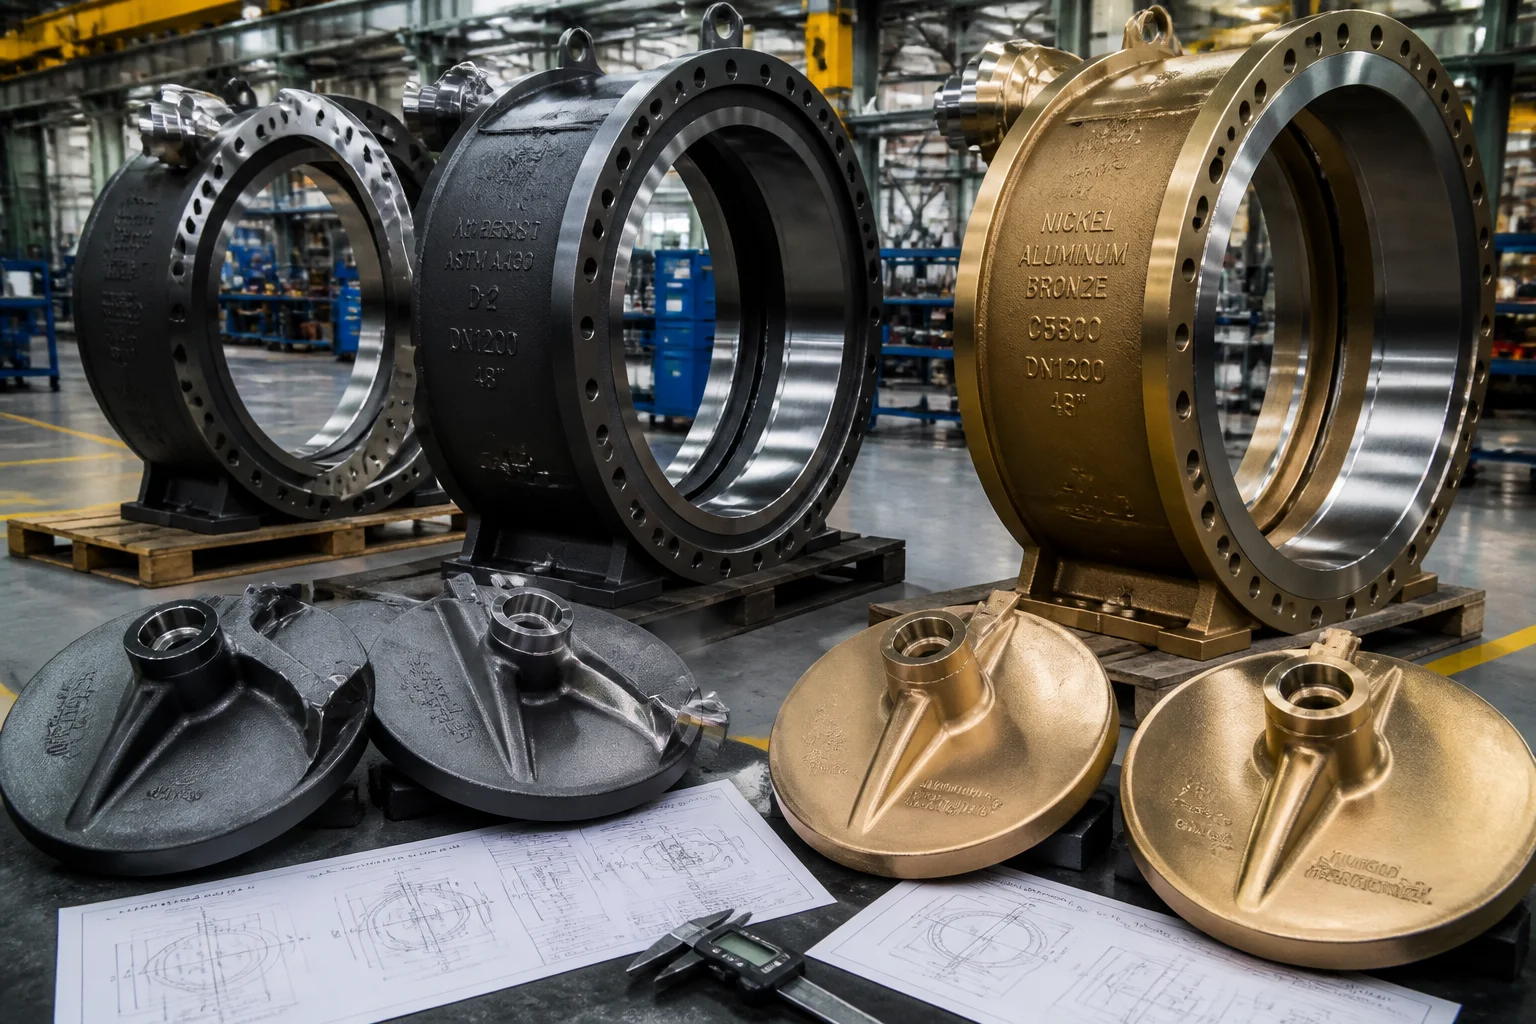
1. Operating Hydraulic Environments & Degradation Modes
                     ┌──────────────────────────────────────────────┐
                     │ High-Volume Saline Water Flow (DN600-DN3000) │
                     └──────────────────────┬───────────────────────┘
                                            │
        ┌───────────────────────────────────┼───────────────────────────────────┐
        ▼                                   ▼                                   ▼
┌───────────────────────────────┐ ┌───────────────────────────────┐ ┌───────────────────────────────┐
│ Chloride Pitting & Crevice    │ │ Cavitation Jet Erosion        │ │ Elastic Seat Deformation      │
│ (Hypersaline brine attacking  │ │ (High-velocity throttling     │ │ (Body ovalization under line  │
│  disc pivot trunnions)        │ │  eroding metal seat profiles) │ │  pressure causing seal bypass)│
└───────────────────────────────┘ └───────────────────────────────┘ └───────────────────────────────┘| Water Valve Application | Service Water Chemistry | Dominant Failure Mode | Material Grade Solution |
|---|---|---|---|
| SWRO Desalination Intake Butterfly Valves | Raw Coastal Seawater () + biofouling | Marine galvanic corrosion, de-aluminization | Nickel-Aluminum Bronze (ASTM B148 C95800 / Cu3) |
| High-Pressure Brine Reject Valves | Hypersaline Brine ( / ) | Extreme crevice corrosion, pitting washout | Super Duplex Stainless Steel (2507 / ASTM A890 5A) |
| Municipal Potable Water Butterfly Valves | Treated Fresh Water () / | Internal tuberculation rust, disc seal leaking | Ductile Iron (EN-GJS-400-15) + Fusion-Bonded Epoxy (FBE) |
| Industrial Wastewater & Slurry Valves | Acidic / Alkaline Effluent () | Chemical leaching, sliding slurry abrasion | Ni-Resist Ductile Iron (ASTM A439 D-2 / D-2B) |
2. Water & Desalination Alloy Metallurgy Hierarchy
Material Selection Matrix for Large-Diameter Water Castings:
| Alloy Family | Material Standard / Equivalent | Nominal Chemical Composition (wt%) | Microstructure & Matrix | Mechanical Properties | Application Role |
|---|---|---|---|---|---|
| Austenitic Ni-Resist Ductile Iron | ASTM A439 Type D-2 / EN-GJSA-XNiCr20-2 | Spheroidal Graphite in Stable FCC Austenite Matrix | High-salinity brine valves, wastewater pumps, sewage treatment discs | ||
| Nickel-Aluminum Bronze (NAB) | ASTM B148 C95800 / EN 1982 CC333G | Intermetallic Phase Matrix | Seawater intake butterfly discs, marine cooling water isolation valves | ||
| High-Ductility Nodular Iron | EN-GJS-400-15 / GB QT400-15 | Fully Ferritic Matrix ( Ferrite) | High-pressure municipal potable water bodies, rubber-lined gate valves | ||
| Super Duplex Stainless | ASTM A890 5A (CE3MN / 2507) | 50/50 Austenite-Ferrite Dual Phase (PREN ) | High-pressure SWRO membrane feed and energy recovery valves |
Metallurgical Focus: Ni-Resist Ductile Iron (ASTM A439 D-2)
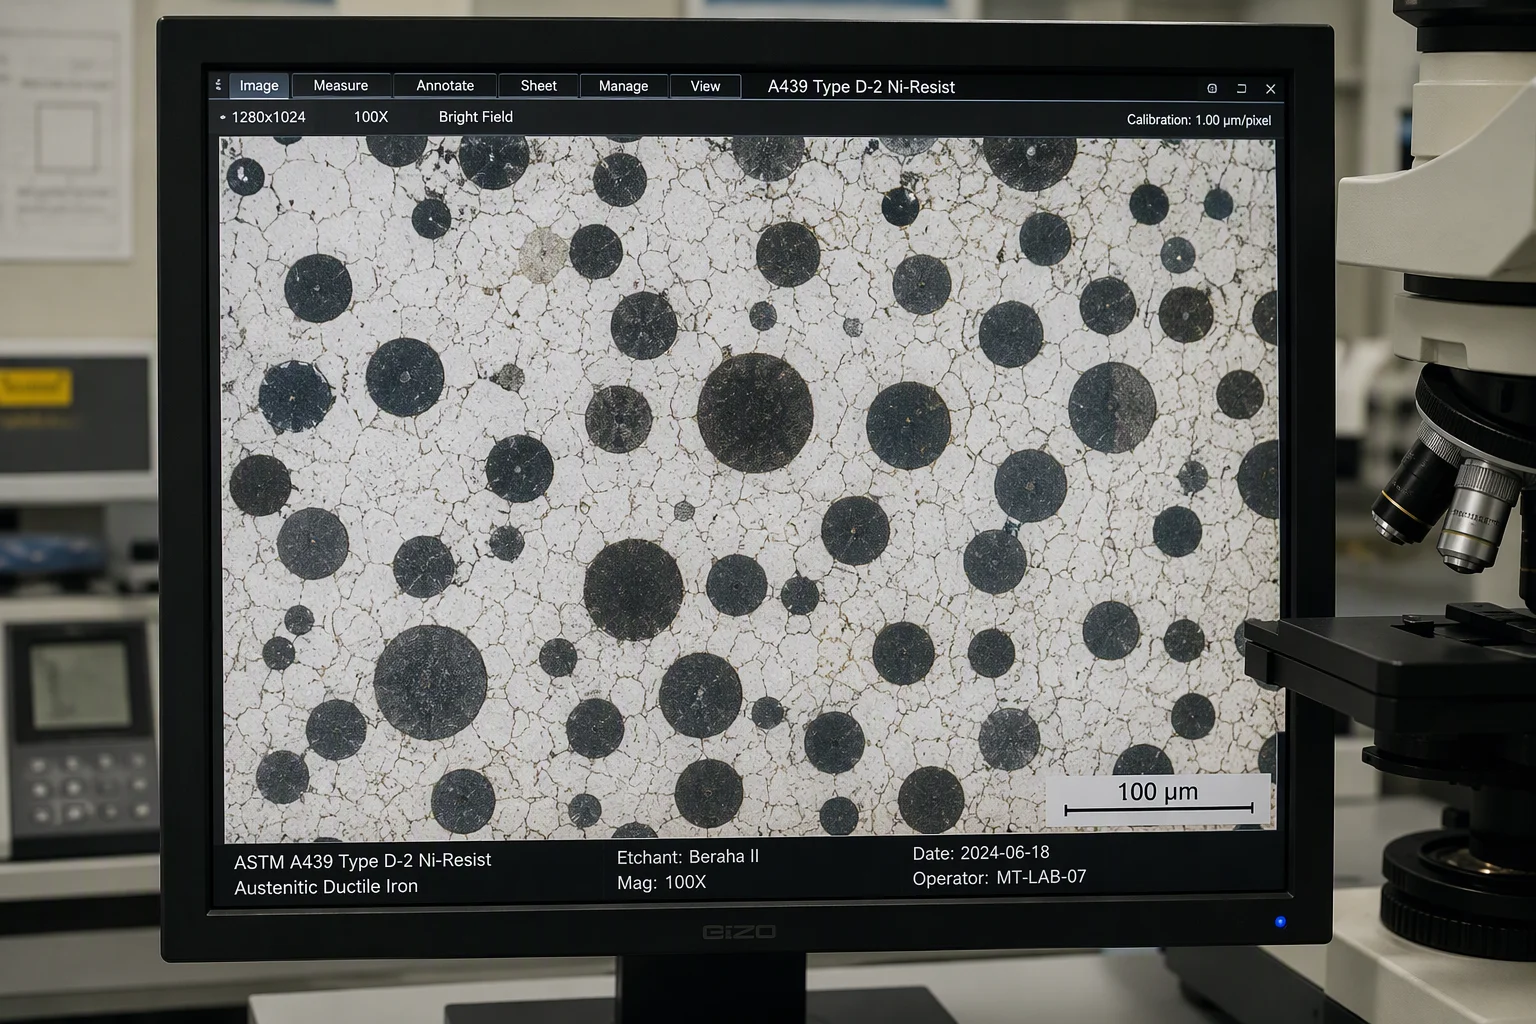
Adding Nickel stabilizes a fully austenitic face-centered cubic (FCC) iron matrix at room temperature, which forms a dense, self-healing oxide film that resists galvanic corrosion in saline waters while the spheroidal graphite nodules provide natural galling resistance and vibration damping during high-velocity throttling.
3. DFM Casting Architecture for Large Valve Bodies (DN600–DN3000)
Casting massive 3 to 15-ton valve bodies and double-flanged discs requires specialized mold stiffness and thermal modulus risering:
┌─────────────────────────────────────────────────────────────┐
│ 1. 3D Precision Master Tooling & Wooden Segmented Patterns  │
│    • Hydrodynamic disc profile with low head-loss coefficient│
├─────────────────────────────────────────────────────────────┤
│ 2. Automated Furan Resin Sand Molding with Zircon Wash      │
│    • High-rigidity molds prevent body flange distortion     │
├─────────────────────────────────────────────────────────────┤
│ 3. Precision Dovetail Lining Retention Grooves              │
│    • Cast-in or CNC-machined dovetail retention slots for   │
│      vulcanized EPDM / NBR rubber body lining               │
├─────────────────────────────────────────────────────────────┤
│ 4. Directional Feeder Risers over Trunnion Shaft Bosses     │
│    • High thermal modulus feeder risers prevent shrinkage   │
│      porosity along heavy shaft bearing bores               │
└─────────────────────────────────────────────────────────────┘
4. Large-Envelope Vertical CNC Turning & Disc Profiling
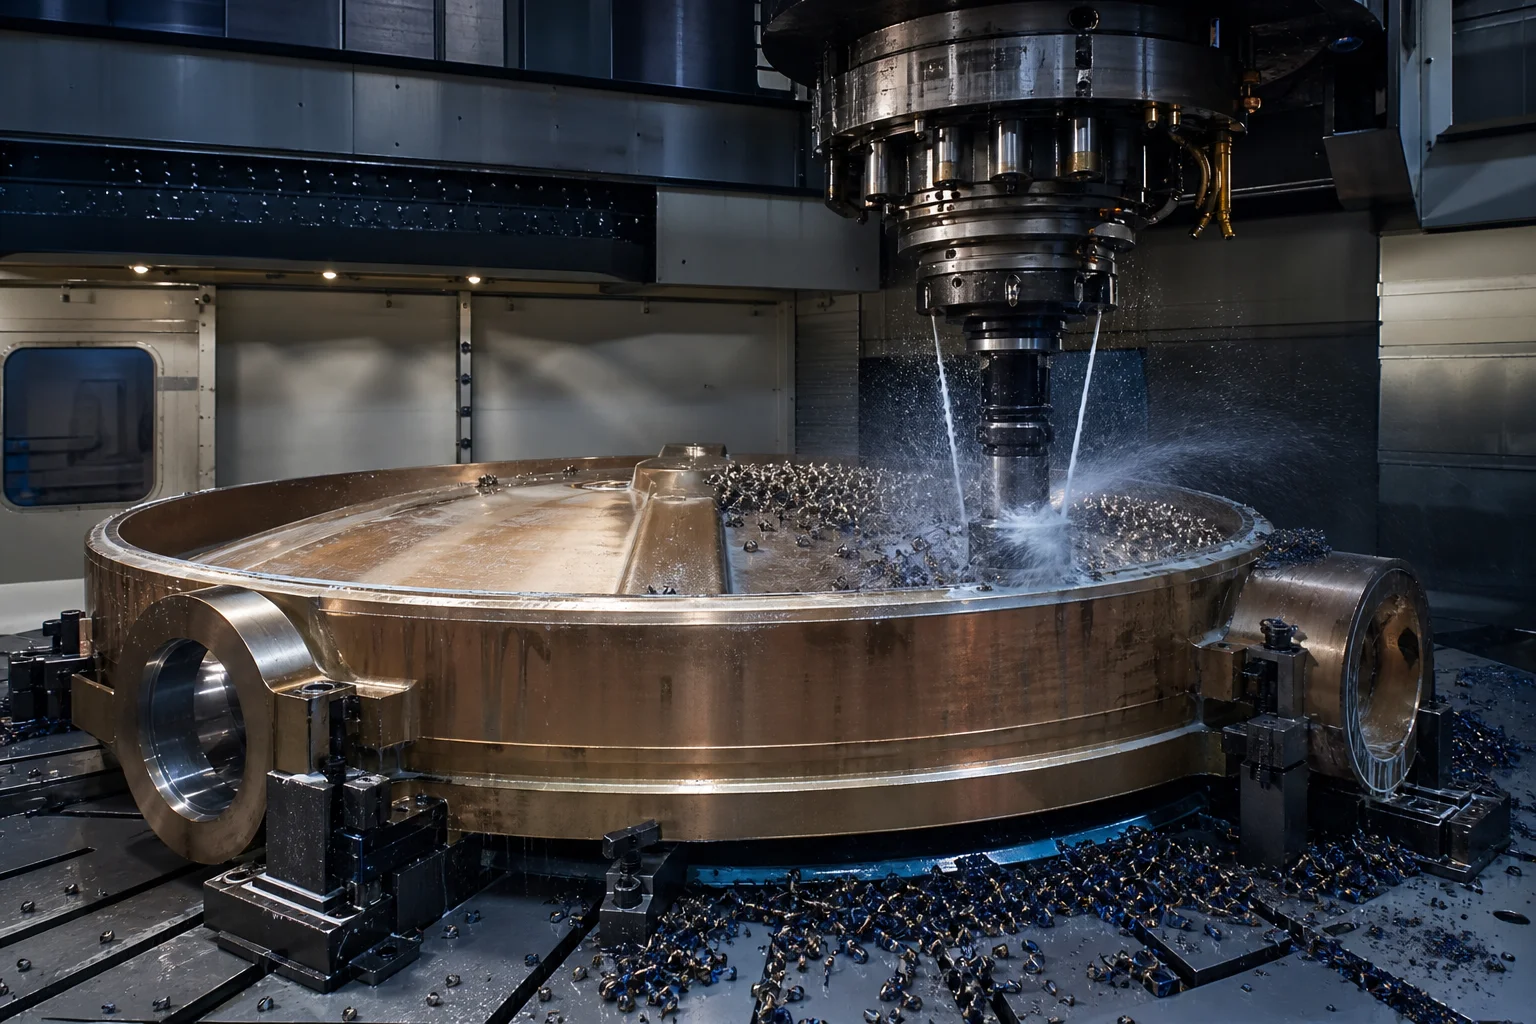
Large butterfly valve sealing depends on sub-millimeter concentricity between the body seat bore and the eccentric disc sealing edge:
        ┌───────────────────────────────────────────────────────┐
        │ 1. Full Normalizing / Annealing Stress Relief         │
        │ • Eliminates residual stresses; stabilizes roundness  │
        └──────────────────────────┬────────────────────────────┘
                                   │
                                   ▼
        ┌───────────────────────────────────────────────────────┐
        │ 2. Large 6-Meter CNC Vertical Turning Lathe (VTL)     │
        │ • Precision turning of body seat bore and raised face │
        │   flanges (Concentricity within $\le 0.040\text{ mm}$)│
        └──────────────────────────┬────────────────────────────┘
                                   │
                                   ▼
        ┌───────────────────────────────────────────────────────┐
        │ 3. 5-Axis Multi-Axis CNC Disc Sealing Edge Milling    │
        │ • Precision milling of double/triple eccentric disc   │
        │   spherical profile ($Ra \le 0.4\text{ µm}$)          │
        │ • Horizontal in-line boring of dual shaft trunnions   │
        │   (Coaxiality $\le 0.025\text{ mm}$ across 3 meters)  │
        └───────────────────────────────────────────────────────┘
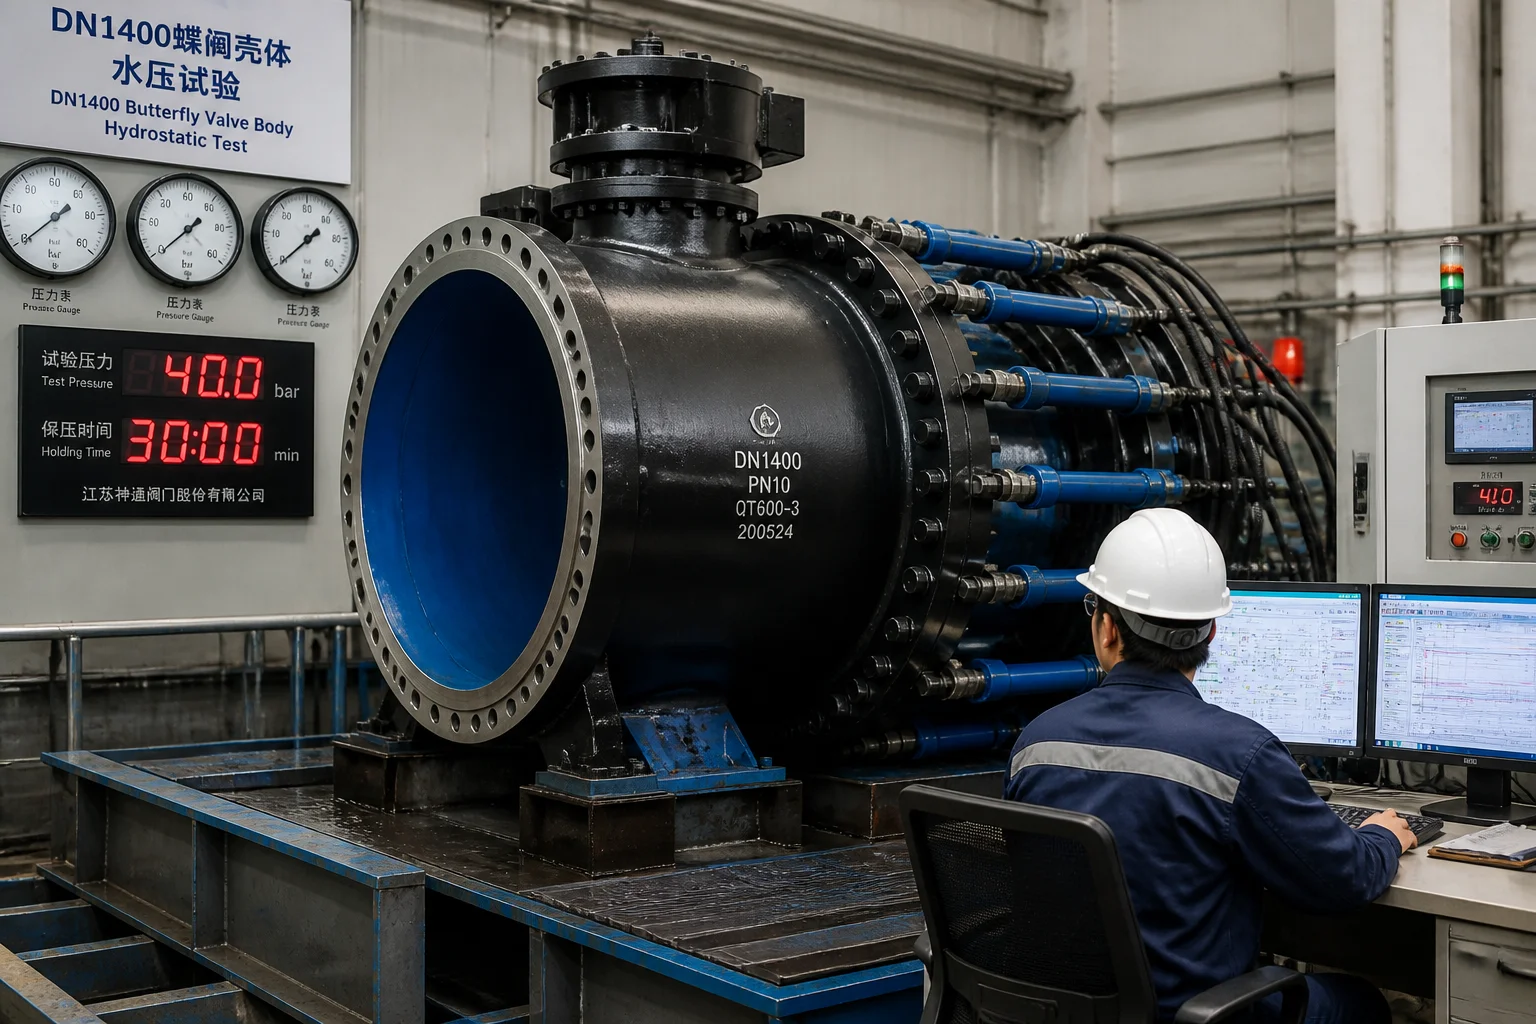
5. Hydrostatic Pressure Proof Testing & Sealing Standards (AWWA / EN 593)
| Quality Test Category | Standard / Test Specification | Test Parameter & Acceptance Criteria |
|---|---|---|
| Hydrostatic Shell Proof Test | AWWA C504 / EN 12266-1 / ISO 5208 | rated cold working pressure () held for ; zero leakage |
| Bi-Directional Seat Leak Test | AWWA C504 / EN 12266-1 Rate A | Tested in both forward and reverse pressure directions; Zero Allowable Bubble Leakage (Rate A) |
| Coating Holiday Spark Test | NACE SP0188 / ISO 29601 | High-voltage spark test () across 100% of internal FBE epoxy or EPDM lining; zero pinhole sparks |
| Ultrasonic Testing (UT) | EN 12680-3 Class 3 / ASTM A609 | 100% volumetric scan on shaft trunnions, disc hubs, and body neck flanges; zero voids |
| Magnetic Particle Testing (MT) | ISO 9934 / ASTM E709 (Fluorescent) | 100% coverage of trunnion fillets and flange transitions; zero linear crack indications |
6. Large Valve Casting Capabilities at Dandong City Pengxin Machinery Co., Ltd.
Manufacturing large-diameter water and desalination valve castings demands heavy induction melting, precision pit molding facilities, large CNC vertical turning lathes, and automated pressure testing bays.
Dandong City Pengxin Machinery Co., Ltd. delivers fully certified, turnkey finished waterworks and desalination valve castings:
- Comprehensive Alloy Expertise: Certified production of Ni-Resist Ductile Iron (ASTM A439 D-2), Nickel-Aluminum Bronze (C95800), Ferritic Ductile Iron (EN-GJS-400-15), and Super Duplex Stainless (2507).
- Large-Diameter Capacity: 80,000 m² facility with heavy overhead cranes capable of casting and machining single valve bodies and discs from DN600 up to DN3000 (weights from 1 ton up to 25 tons).
- Large-Envelope CNC Machining: Large 6-meter to 8-meter CNC vertical turning lathes and floor-type horizontal boring mills delivering trunnion coaxiality .
- Protective Coating & Lining Integration: Dedicated blast-cleaning and automated Fusion-Bonded Epoxy (FBE DFT) and vulcanized rubber lining application bays.
- Complete Quality Certification: ISO 9001 certified, providing full EN 10204 3.1 & 3.2 material test certificates, 100% UT/MT reports, and bi-directional hydrostatic test charts.
Conclusion
Large industrial water treatment and seawater desalination valve castings represent the vital hydraulic conduits of global water security. Operating for decades in hypersaline seawater and high-flow potable water pipelines demands corrosion-resistant metallurgy (Ni-Resist D-2, NAB C95800, and lined ductile iron), precision large-envelope vertical CNC turning, and verified zero-leakage bi-directional hydrostatic testing per AWWA C504 and EN 593.
Partnering with an experienced, integrated heavy casting and precision machining powerhouse ensures that your municipal and desalination valve systems operate with maximum hydraulic efficiency, zero leakage, and decades of reliable service.
Contact Dandong City Pengxin Machinery Co., Ltd. to submit your large-diameter valve body or disc drawings.
Dandong City Pengxin Machinery Co., Ltd. — Heavy Castings and Precision Machining, Since 1958.
Table of Contents
- 1. Operating Hydraulic Environments & Degradation Modes
- 2. Water & Desalination Alloy Metallurgy Hierarchy
- 3. DFM Casting Architecture for Large Valve Bodies (DN600–DN3000)
- 4. Large-Envelope Vertical CNC Turning & Disc Profiling
- 5. Hydrostatic Pressure Proof Testing & Sealing Standards (AWWA / EN 593)
- 6. Large Valve Casting Capabilities at Dandong City Pengxin Machinery Co., Ltd.
- Conclusion