
 EN
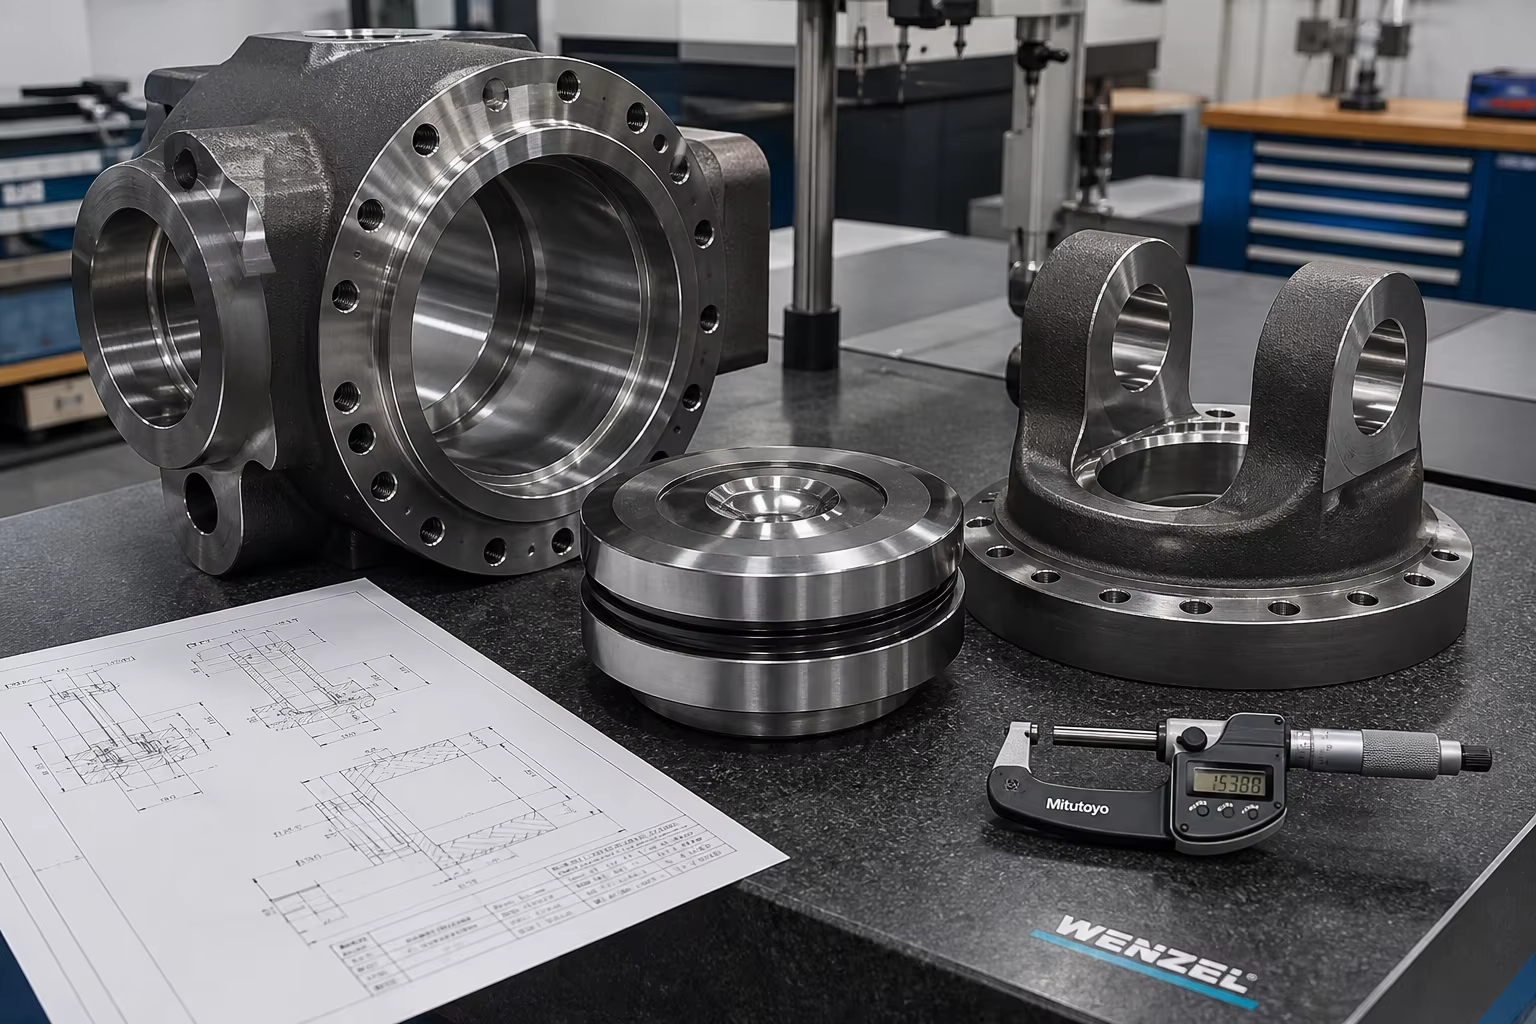
Meta Description: An in-depth technical guide to heavy hydraulic cylinder and industrial forging press castings. Learn alloy steel selection (ASTM A27 / A216 WCB / 34CrMo4), heavy ductile iron (QT600-3), directional feeding for 350-700 bar fluid containment, deep-hole CNC boring, and hydrostatic proof testing.
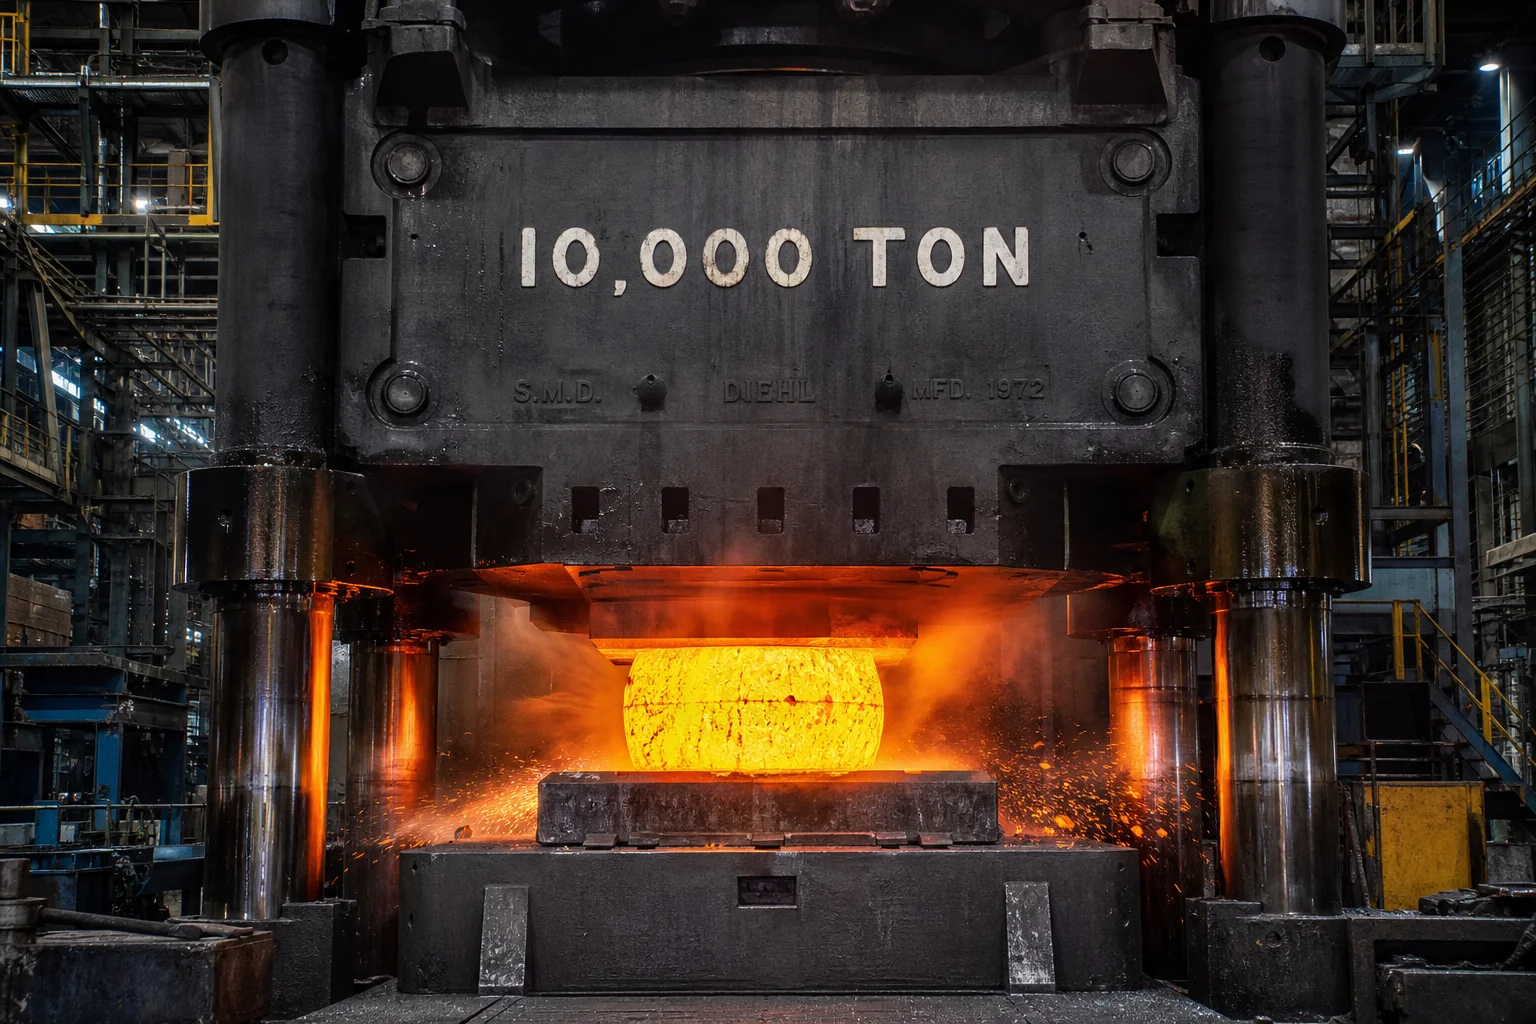
In heavy open-die forging presses, high-tonnage plastic injection molding machines, metal die-casting machines, and offshore marine jacking platforms, hydraulic power transmission components operate under immense hydrostatic loads. Massive hydraulic cylinder bodies, front cylinder heads, piston caps, bottom clevis bases, and moving press platens are subjected to continuous dynamic fluid pressures ranging from (), generating multi-thousand-ton clamping and forging forces.
Under these punishing conditions, hydraulic pressure-boundary components endure continuous cyclic pressure surges, high-amplitude pressure-spike shocks, multi-axial hoop stresses, and severe hydraulic fluid erosion.
A single internal shrinkage cavity, micro-porosity cluster, or slag inclusion within a 15-ton cylinder base will cause high-pressure hydraulic fluid weeping, premature fatigue rupture, or catastrophic platen fracturing under 10,000 tons of forging impact.
Achieving absolute fluid containment requires specialized foundry engineering: casting High-Integrity Carbon-Manganese Steels (ASTM A216 WCB / GS-20Mn5), high-strength Alloy Cast Steels (34CrMo4 / 42CrMo4), and Heavy Hydraulic Ductile Iron (QT500-7 / QT600-3), backed by directional thermal feeding simulation, deep-hole CNC internal boring with mirror-finish honing (), and high-pressure hydrostatic proof testing.
This technical guide details the metallurgy, solidification risering, deep-hole machining, and quality assurance standards for heavy hydraulic and press castings.
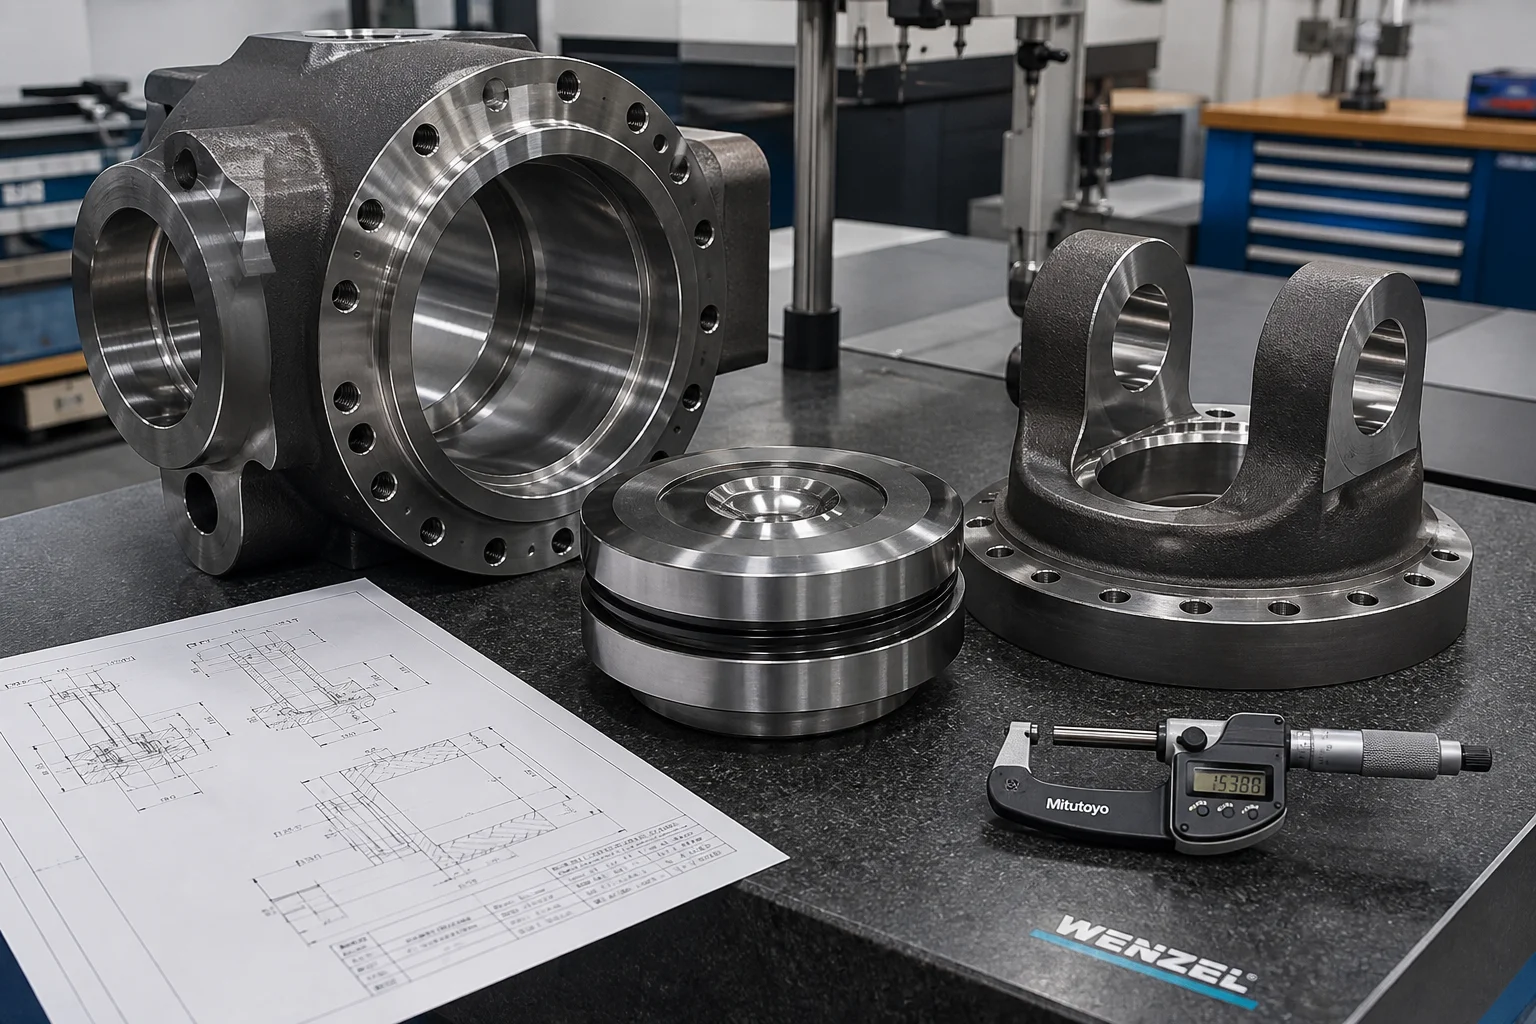
1. Operating Pressure Fields & Mechanical Failure Modes
                     ┌──────────────────────────────────────────────┐
                     │ Ultra-High Dynamic Hydraulic Pressure        │
                     │ (350 bar – 700 bar / >10,000 Ton Force)      │
                     └──────────────────────┬───────────────────────┘
                                            │
        ┌───────────────────────────────────┼───────────────────────────────────┐
        ▼                                   ▼                                   ▼
┌───────────────────────────────┐ ┌───────────────────────────────┐ ┌───────────────────────────────┐
│ High-Cycle Pressure Fatigue   │ │ Micro-Porosity Fluid Weeping  │ │ Press Platen Bending Deflect  │
│ (Pulsating hoop stress causing│ │ (Subsurface micro-shrinkage   │ │ (Uneven die load causing      │
│  fillet fatigue cracking)     │ │  channeling pressurized oil)  │ │  central platen cracking)     │
└───────────────────────────────┘ └───────────────────────────────┘ └───────────────────────────────┘| Hydraulic Component | Operating Pressure & Dynamic Load | Primary Failure Mode | Material Solution |
|---|---|---|---|
| Main Forging Cylinder Body | cyclic hydraulic pressure + pressure spikes | Wall hoop-stress yielding, barrel fatigue rupture | High-Strength Cast Alloy Steel (34CrMo4 / 42CrMo4 Q&T) |
| Front Cylinder Head / Gland | High tensile tie-rod preload + high-pressure seal friction | Flange bending shear, seal gland blowout | Forging-Grade Cast Carbon Steel (ASTM A216 WCB / GS-20Mn5) |
| Piston Cap & Bottom Clevis | Direct compressive impact () + pin shear | Clevis lug bending fatigue, pin bore galling | Heavy Ductile Iron (QT600-3) / Cast Alloy Steel (ASTM A148) |
| Moving Press Platen (10–30 Tons) | Multi-point die clamping force + severe 3-point bending | Centerline platen sagging, T-slot breakout | Rigid Heavy Cast Steel (GS-20Mn5) / Pearlitic Ductile Iron (QT700-2) |
2. Pressure-Boundary Alloy Metallurgy & Material Selection
Material Selection Matrix for Heavy Fluid Power Castings:
| Material Family | Standard / Specification | Chemical Composition (wt%) | Heat Treatment | Mechanical Properties | Ideal Fluid Power Application |
|---|---|---|---|---|---|
| Cast Carbon-Manganese Steel | ASTM A216 WCB / EN 10293 GS-20Mn5 | Normalized & Tempered | Standard hydraulic cylinder heads, press platens, clevis bases | ||
| High-Strength Cr-Mo Cast Steel | ASTM A148 Gr 105-85 / 34CrMo4 (1.7220) | Quenched & Tempered (Q&T) | High-pressure forging press cylinders (), tie-rod nuts | ||
| Heavy Hydraulic Ductile Iron | EN-GJS-600-3 / GB QT600-3 | As-Cast / Normalized | Heavy piston heads, valve manifold blocks, hydraulic pump bodies | ||
| Low-Temperature Pressure Steel | ASTM A352 LCC / 1.6220 | Quenched & Tempered | Offshore marine jacking cylinders, subsea accumulator bodies |
Metallurgical Purity & Deoxidation:
High hydrostatic pressures will force mineral hydraulic oils through micro-shrinkage channels connecting non-metallic inclusion clusters.
- Vacuum Degassing & Ladle Refining: Molten steel undergoes argon stirring and calcium treatment to spheroidize inclusions and reduce dissolved gas ().
- Phosphorus and Sulfur Restriction: to eliminate hot tearing along heavy flange intersections.
3. Directional Solidification Modeling for Thick-Wall Pressure Castings
Hydraulic cylinders and press platens feature massive wall thickness transitions: cylinder barrels () meet heavy mounting flanges and closed bottom bases ().
┌─────────────────────────────────────────────────────────────┐
│ Directional Solidification Strategy for Pressure Castings   │
├─────────────────────────────────────────────────────────────┤
│ 1. Computer-Aided Thermodynamic Simulation (MAGMA / ProCAST)│
│    • Identifies isolated hot-spots at barrel-to-base fillets│
├─────────────────────────────────────────────────────────────┤
│ 2. Strategic Insulated Exothermic Feeder Sleeves             │
│    • High-efficiency exothermic risers over thick bottom hub │
│    • Feeder Modulus $M_{\text{feeder}} \ge 1.4 \times M_{\text{wall}}$│
├─────────────────────────────────────────────────────────────┤
│ 3. Internal Steel Chills at Critical Flange Fillets         │
│    • Forces rapid directional freezing from barrel to riser │
│    • Eliminates centerline spongy shrinkage micro-porosity  │
├─────────────────────────────────────────────────────────────┤
│ 4. Heavy-Compaction Furan Resin No-Bake Sand Molding        │
│    • Rigid mold walls prevent ferrostatic mold dilation     │
└─────────────────────────────────────────────────────────────┘
4. Deep-Hole CNC Machining & Superfinishing
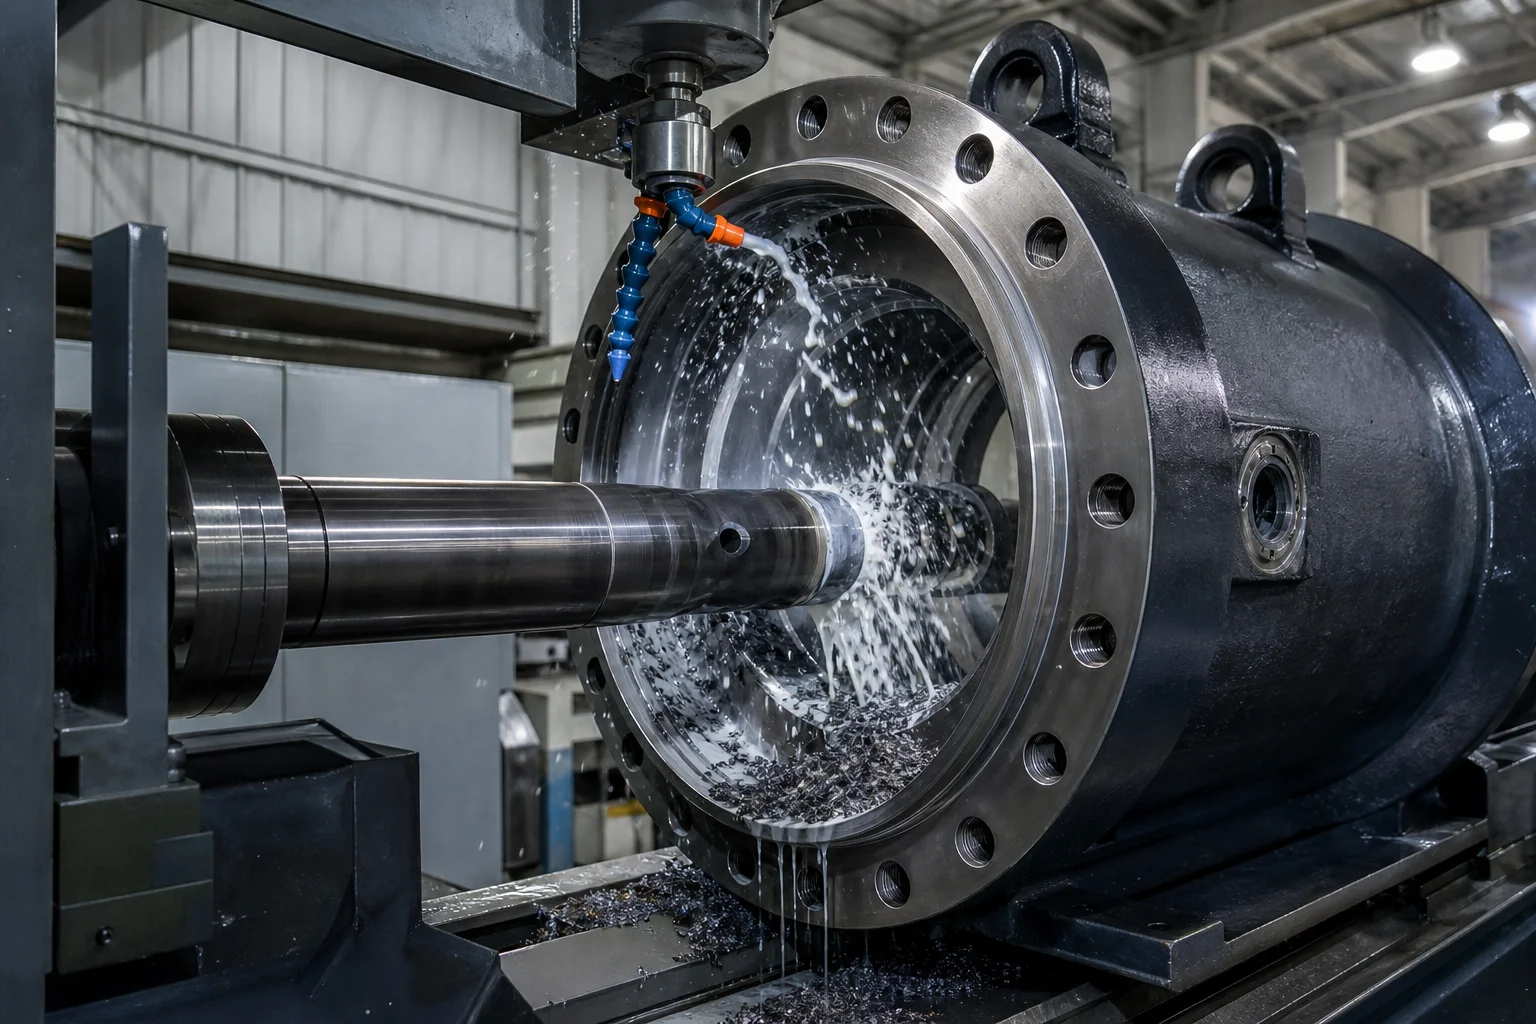
Hydraulic cylinder bores and seal grooves must meet extreme dimensional and surface finish tolerances to prevent seal extrusion and oil bypass:
Precision CNC Operations:
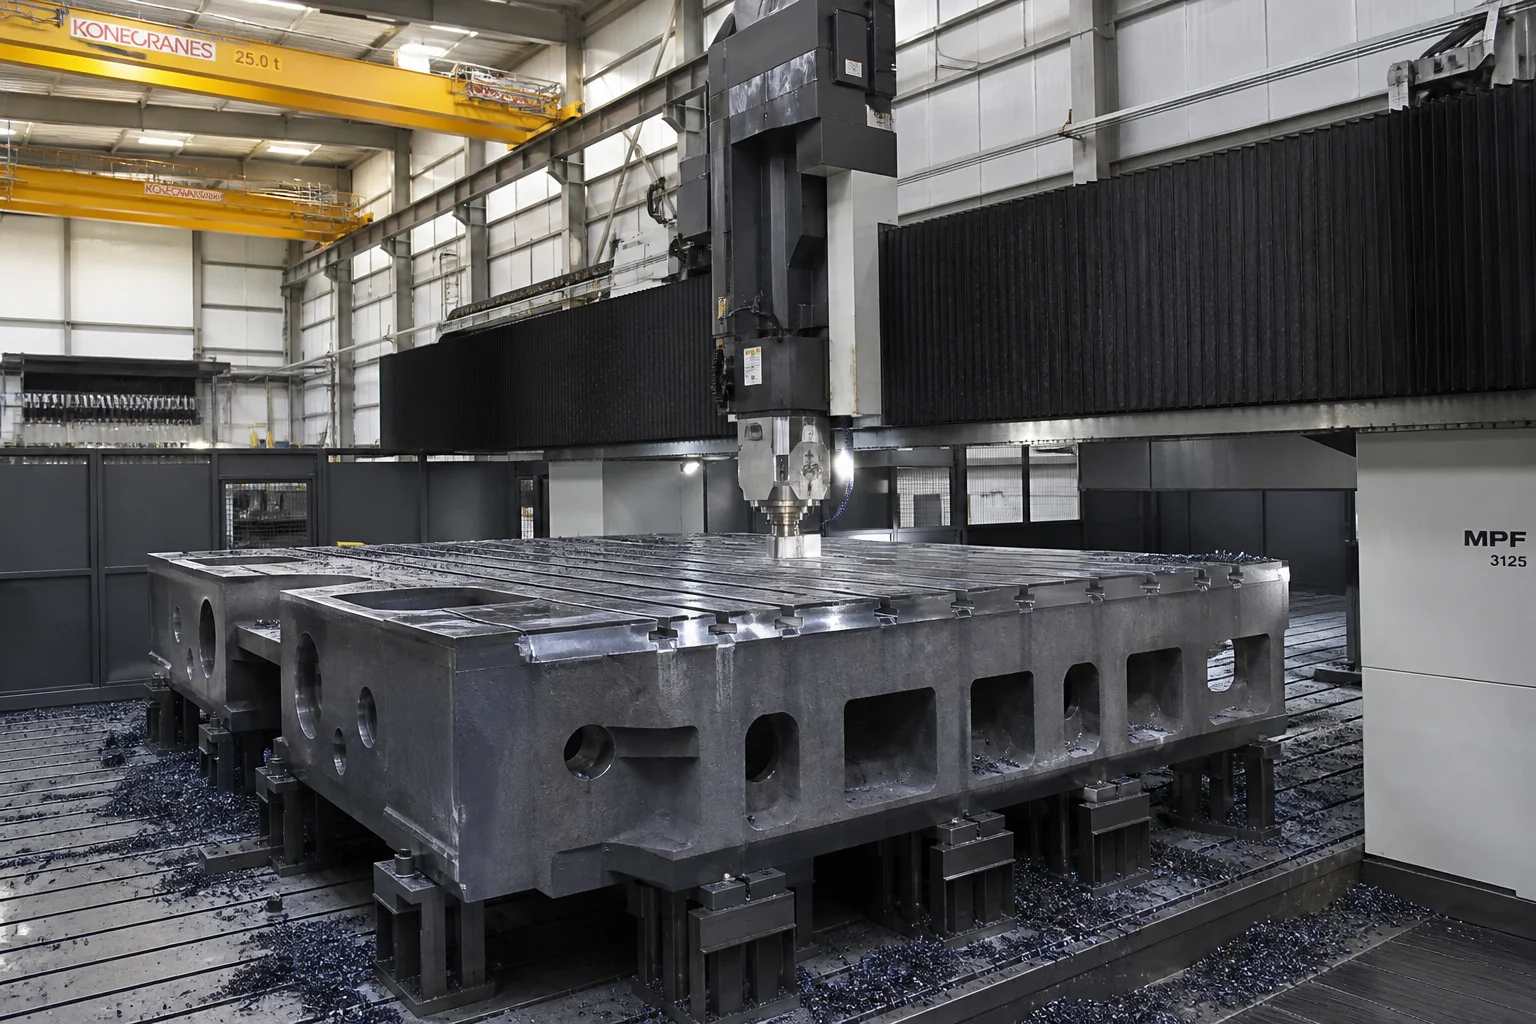
- CNC Horizontal Deep-Hole Boring: Boring cylinder barrels up to 6 meters in length and bores up to 1,200 mm diameter on heavy CNC horizontal boring machines. Bore straightness and roundness are held within .
- Internal Roller Burnishing & Honing: Cylinder internal seal sliding surfaces are precision honed and diamond-roller burnished to achieve an ultra-smooth finish of , maximizing polyurethane and PTFE seal longevity.
- Flange O-Ring & SAE Port Machining: Precision CNC milling of high-pressure O-ring face seal grooves () and SAE 4-bolt flange port threads.
- Platen T-Slot & Guide Bushing Machining: Large CNC gantry milling centers machine DIN 650 T-slots and press guide bushing bores, holding guide rail parallelism within .
5. Hydrostatic Proof Testing & Quality Verification
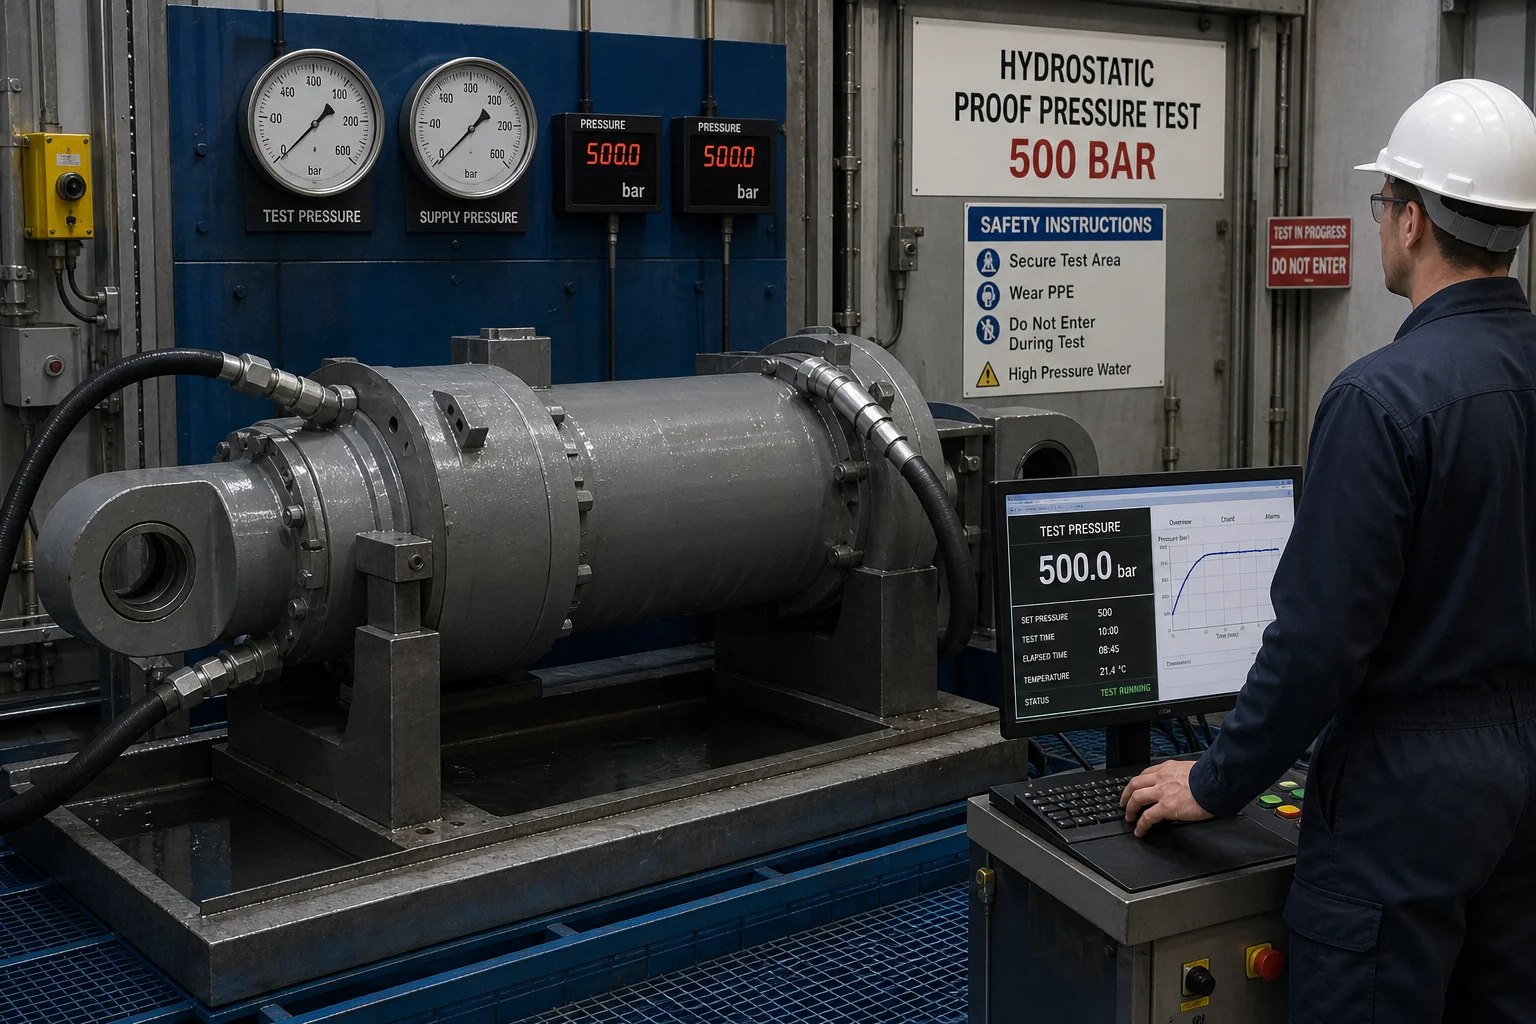
Every pressure-boundary casting undergoes rigorous hydrostatic proof pressure testing before leaving the factory:
        ┌───────────────────────────────────────────────────────┐
        │ 100% Volumetric Ultrasonic Testing (EN 10228-3 Cl 3)  │
        └──────────────────────────┬────────────────────────────┘
                                   │
        ┌──────────────────────────┴───────────────────────────┐
        ▼                                                      ▼
┌───────────────────────────────┐              ┌───────────────────────────────┐
│ Full Hydrostatic Proof Test   │              │ Magnetic Particle (MT) Scan   │
│ • Pressurized to 1.5× design  │              │ • 100% inspection of seal     │
│   working pressure (>500 bar) │              │   faces, tie-rod fillets, and │
│ • 30-minute hold time         │              │   flange radii                │
│ • Digital pressure log        │              │ • Zero linear crack defects   │
│ • Zero pressure drop / weep   │              │                               │
└───────────────────────────────┘              └───────────────────────────────┘
6. Comprehensive Quality Assurance Standards
| Inspection Parameter | Testing Standard | Acceptance Criteria |
|---|---|---|
| Hydrostatic Proof Pressure | ISO 19973 / ASME Sec VIII Div 1 | design pressure held for ; zero pressure decay, zero weeping |
| Ultrasonic Testing (UT) | EN 10228-3 Class 3 / ASTM A609 Level 1 | 100% scan on cylinder bases, heads, and platens; zero critical shrinkage cavities |
| Magnetic Particle Testing (MT) | EN 10228-1 / ASTM E709 (Fluorescent) | 100% coverage of seal grooves, tie-rod fillets, and port threads; zero cracks |
| Bore Cylindricity & Surface | Digital Bore Micrometer & Surface Profilometer | Bore roundness ; surface roughness |
| Tensile & Impact Testing | ISO 6892-1 / ASTM E23 on attached coupons | Verified ; Charpy impact at ( at for LCC) |
7. Heavy Hydraulic Casting Capabilities at Dandong City Pengxin Machinery Co., Ltd.
Delivering large hydraulic cylinders and press castings demands heavy crane capacity, advanced induction melting and vacuum degassing, deep-hole boring lathes, and dedicated high-pressure hydrostatic test bays.
Dandong City Pengxin Machinery Co., Ltd. delivers fully certified, turnkey heavy hydraulic and press castings:
- Comprehensive Material Capability: Certified casting of ASTM A216 WCB, GS-20Mn5, 34CrMo4 / 42CrMo4 alloy steels, and heavy hydraulic ductile irons (QT500-7 / QT600-3).
- Heavy Tonnage Infrastructure: 80,000 m² production facility with heavy overhead cranes capable of pouring single castings from 500 kg up to 25 tons.
- Deep-Hole CNC Machining & Honing: Heavy CNC horizontal boring machines and deep-hole honing tools delivering internal bores up to 1,200 mm diameter and lengths up to 6 meters.
- In-House High-Pressure Test Bay: Dedicated hydrostatic testing rigs capable of proof testing up to with automated digital data acquisition.
- Complete Certification: ISO 9001 certified, providing full EN 10204 3.1 & 3.2 material test certificates, 100% UT/MT reports, and hydrostatic test chart records.
Conclusion
Heavy hydraulic cylinder and forging press castings operate at the extreme frontier of fluid power containment and cyclic fatigue. Preventing catastrophic barrel blowouts or platen fractures demands clean steel deoxidation, scientific directional solidification risering, precision deep-hole CNC boring and honing, and unyielding hydrostatic proof testing.
Partnering with an experienced, integrated heavy casting and precision machining powerhouse ensures that your hydraulic presses and fluid power systems operate with maximum safety, power, and reliability.
Contact Dandong City Pengxin Machinery Co., Ltd. to submit your hydraulic cylinder or press component drawings.
Dandong City Pengxin Machinery Co., Ltd. — Heavy Castings and Precision Machining, Since 1958.
Table of Contents
- 1. Operating Pressure Fields & Mechanical Failure Modes
- 2. Pressure-Boundary Alloy Metallurgy & Material Selection
- 3. Directional Solidification Modeling for Thick-Wall Pressure Castings
- 4. Deep-Hole CNC Machining & Superfinishing
- 5. Hydrostatic Proof Testing & Quality Verification
- 6. Comprehensive Quality Assurance Standards
- 7. Heavy Hydraulic Casting Capabilities at Dandong City Pengxin Machinery Co., Ltd.
- Conclusion